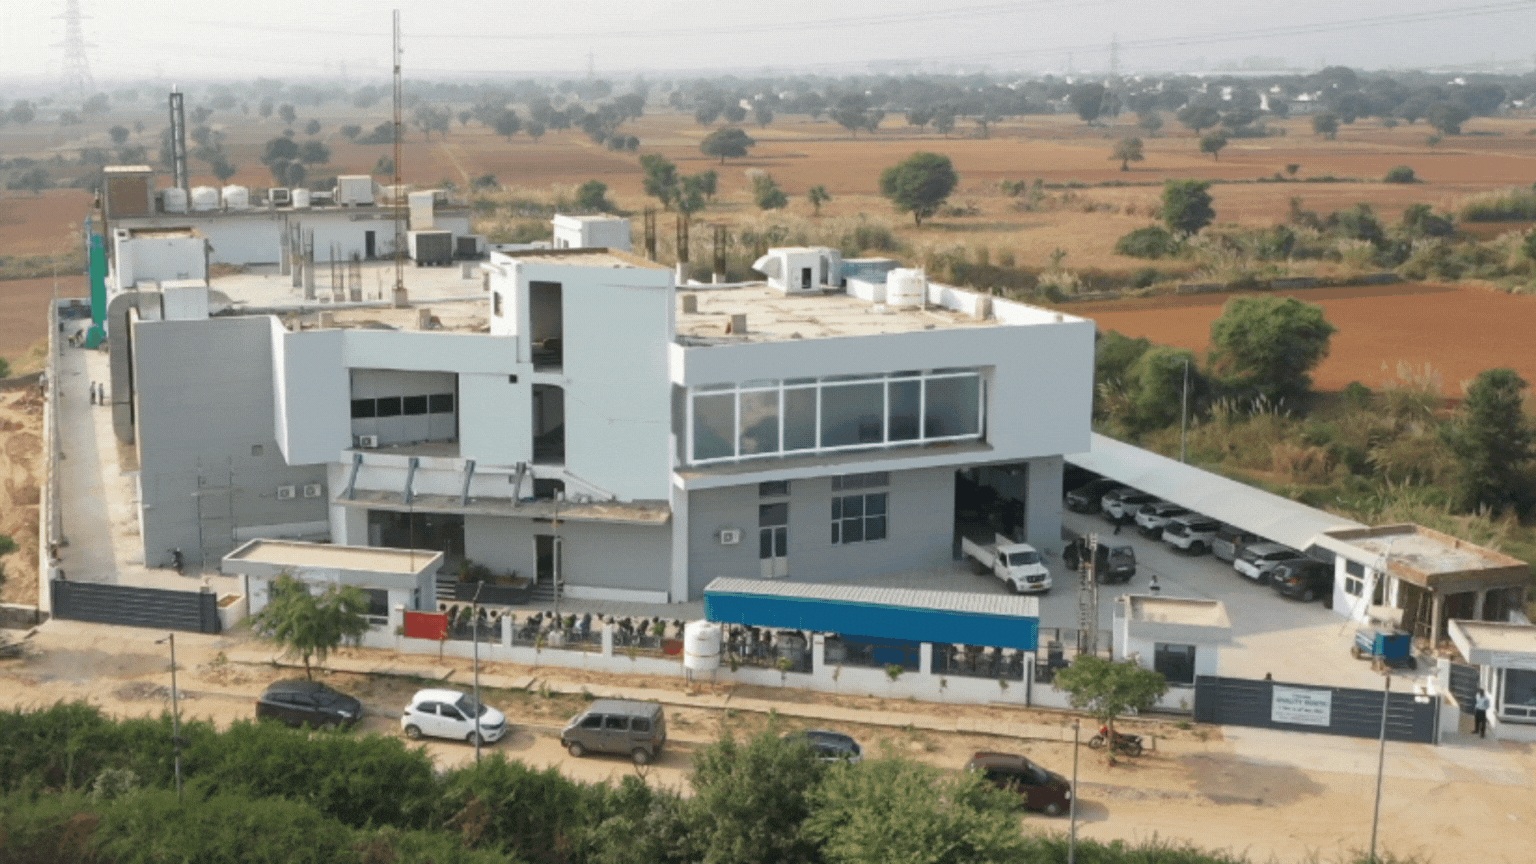
Behind every reel of cable is a plant, and ours sits at EPIP Neemrana in Rajasthan. From conductor to connector, the process is integrated under one roof — which is what lets us hold tolerances and testing consistent across heating cable, specialty wire and harness assembly.
Backward integration is the theme. Making the conductor in the same facility that draws the cable and assembles the harness removes the variability that creeps in when work is handed between suppliers. It also shortens lead times, because scheduling is one plant's decision, not three.
One-hundred-percent end-of-line testing closes the loop. Every harness is tested before it ships, and every cable design is validated in-house against the standards it's built to — quality engineered in at the conductor and proven before dispatch.